A machine performance gap appears when delivered hardware fails to match documented specs. Address it by isolating the variable, checking mechanical alignment, and validating electrical settings. Use acceptance testing to record baseline data before full production begins.
- Document actual output against contract specs before accepting the machine into production.
- Isolate mechanical, electrical, and software variables before requesting a service call.
- Verify spindle runout, table leveling, and drive settings as first-line checks.
- Use acceptance testing to create a baseline for future service disputes.
A machine performance gap is the distance between what the supplier promised and what the machine actually delivers. It is a frequent complaint in imported and domestic woodworking equipment. The gap often shows up in surface finish, cycle time, or dimensional accuracy.
This issue is rarely a single failure. It is usually a combination of setup errors, transport damage, or a mismatch between the buyer’s expectations and the machine’s physical limits.
What is a machine performance gap
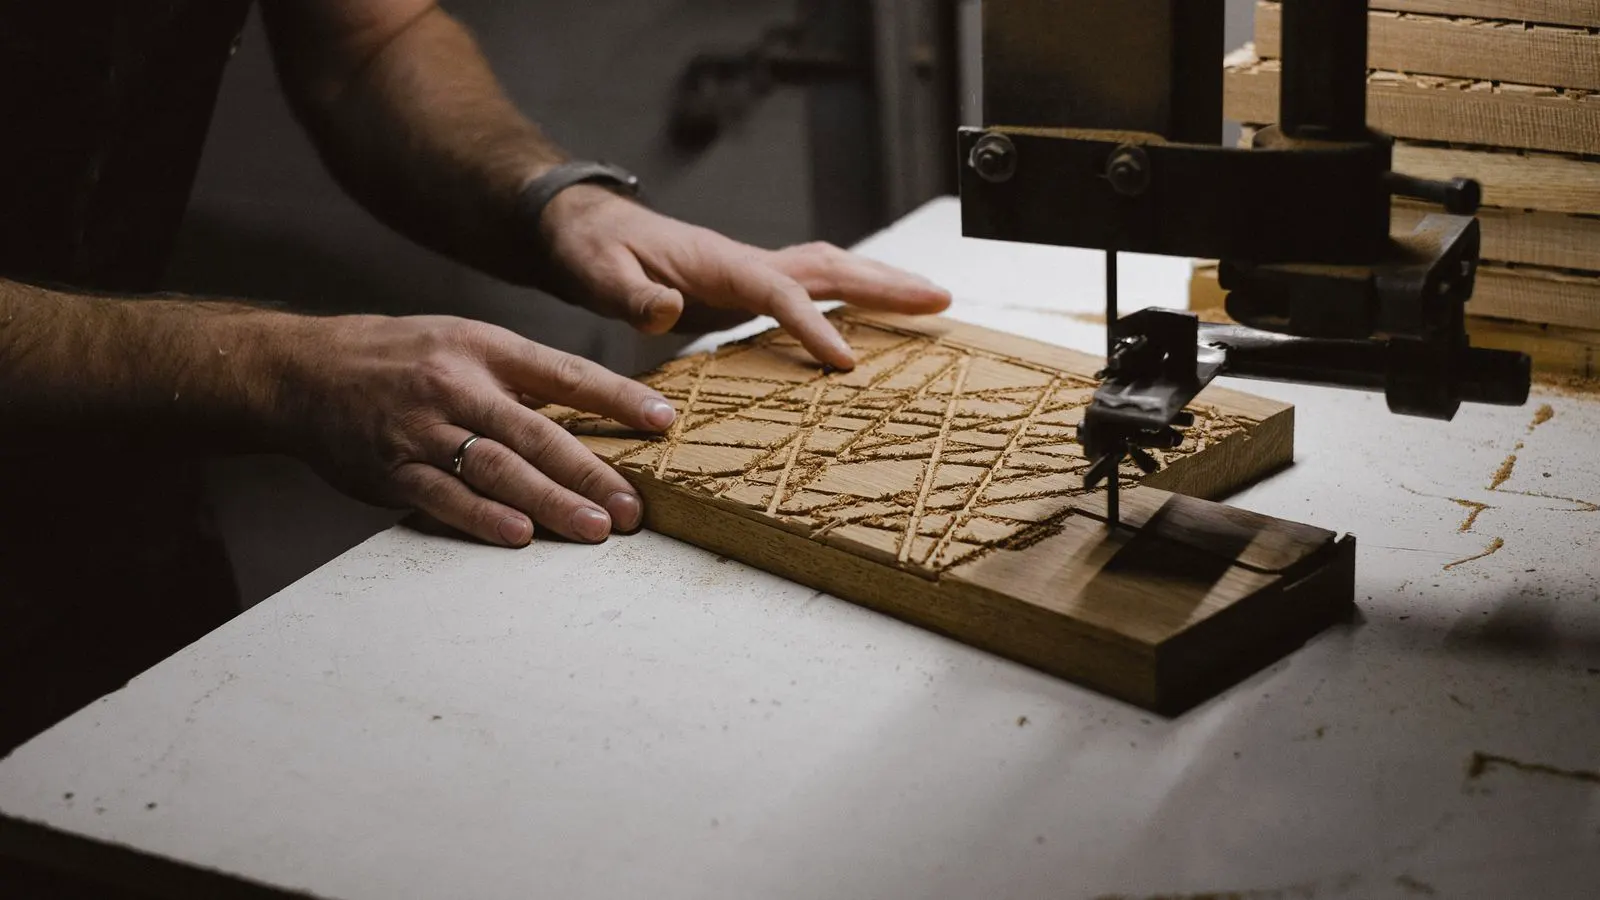
The term covers any measurable drop in output quality or speed relative to the purchase agreement. It includes a CNC router that cuts 0.5 mm slower than rated, a band saw that produces chattering cuts, or a planer that fails to hold a consistent thickness.
The gap is not always a defect. Sometimes the machine meets its specs but the operator does not. Sometimes the specs in the brochure are optimistic. The key is separating a genuine fault from an operational mismatch.
Before calling a technician, define the gap. Measure it. Take a sample of five finished parts. Compare them to a standard. Record the cycle time. Without data, the conversation with the supplier remains vague and unproductive.
Common symptoms of underperformance
Most performance gaps fall into a few visible categories. Surface finish degrades first. Cycle time increases. Dimensional tolerance widens. The machine may also make unusual noises or show signs of overheating.
Identifying the symptom helps narrow the cause. A rough surface finish often points to spindle runout or dull tooling. A slow cycle time usually involves drive settings or software limitations. A loose tolerance suggests mechanical play in the table or axis rails.
| Symptom | Likely cause | What to do |
|---|---|---|
| Rough surface finish on hardwoods | Spindle runout, dull tooling, or excessive table vibration | Measure runout with a dial indicator. Replace or sharpen tools. Check table leveling and fasteners. |
| Cycle time significantly slower than rated | Incorrect feed rate settings, low voltage supply, or software mode limits | Verify electrical supply voltage. Check controller settings for speed limits. Confirm software is not in safe mode. |
| Dimensional accuracy off by 0.3 mm or more | Unlevel table, thermal expansion, or axis backlash | Level the machine on the floor. Check rail lubrication. Run calibration routines in the control panel. |
| Machine overheats during continuous operation | Insufficient cooling airflow, blocked dust extraction, or worn bearings | Clear dust filters and extraction ducts. Check coolant levels. Listen for bearing noise and measure temperature. |
| Chattering cuts on soft materials | Tool overhang, loose collet, or table sag | Reduce tool overhang. Tighten the collet. Check the table for flex under load. |
First line diagnostic checks
Start with the mechanical baseline. A machine that was damaged during transit will not perform like one that was stored properly. Check the floor. If the machine sits on a concrete slab, verify it is level. Use a bubble level along both axes. A machine that is even 0.5 mm out of level on a long table will struggle to hold tolerance.
Next, check the spindle. Spindle runout is a frequent cause of poor finish. Use a dial indicator to measure the runout at the tool holder. Compare the reading to the spec in the manual. If the runout exceeds the limit, the spindle bearing may be worn or the tool holder may be damaged.
Do not assume the tooling is the problem. Replace a known good set of inserts or bits. Run the test again. If the finish improves, the issue was the tooling. If it does not, the machine needs attention.
Check the electrical supply. Woodworking machinery is sensitive to voltage fluctuations. A drop in voltage during heavy cutting loads can slow the spindle and reduce feed consistency. Use a multimeter to verify the line voltage matches the nameplate requirement. Check the power factor if the machine has a high inrush current.
Electrical and software verification
The controller settings are often where the gap hides. A supplier may ship a machine with default settings that are conservative. These settings protect the machine but limit output. Review the controller parameters for feed rate, spindle speed, and acceleration.
Compare the settings to the spec sheet provided with the machine. If the spec sheet lists a maximum feed rate of 12,000 mm/min and the controller is set to 8,000 mm/min, the machine is underperforming by design. This is a configuration issue, not a hardware defect.
Check the software version. Some machines have firmware updates that improve performance or fix bugs. Ask the supplier for the latest release. Verify the machine is running the correct code for the specific material and tooling.
The acceptance test should capture these settings. Record the controller version, the firmware build number, and the parameter file. If the machine underperforms later, you can restore the original configuration or demonstrate that the settings were changed.
Acceptance testing protocol
Acceptance testing is the bridge between delivery and production. It is a structured process to verify that the machine meets the purchase requirements. Do not skip it because the machine looks good and runs smoothly.
Define the test criteria before the supplier leaves. Use the purchase order spec. If the order says the machine must cut 10 mm oak at 15,000 RPM with a surface roughness of 0.05 mm, test for exactly that.
Run a three-part test. First, run an idle cycle to check for unusual noises or errors. Second, run a standard cut on a representative material. Measure the dimensions and finish. Third, run a stress cycle at the maximum rated speed for thirty minutes. Check temperature and vibration.
Record all data. Take photos of the finished parts. Save the controller logs. This documentation protects the buyer. If the machine fails within the warranty period, the acceptance test data proves the baseline. It also helps the supplier identify the issue faster.
If the machine fails the acceptance test, do not sign the final delivery note. Note the specific gap on the document. The supplier is usually required to rectify the issue before the buyer takes full responsibility.
Preventing gaps in future purchases
Prevention starts before the machine arrives. Review the supplier’s documentation carefully. Ask for the parameter file and the software manual. Verify that the spec sheet matches the machine model and configuration.
Check the transport packaging. Woodworking machines are heavy and sensitive. A missing shock absorber or a loose component can cause a gap. Inspect the machine on arrival. Look for dents, cracks, or loose fasteners.
Train the operator before the first production run. A gap that looks like a machine defect is often an operator error. Ensure the operator understands the controller, the tooling setup, and the material limits.
Build a relationship with the supplier’s service team. Know who to call. Have the service manual and parts list on hand. A quick phone call can often resolve a setting issue without a truck and a technician.
When to escalate the issue
If the gap persists after mechanical, electrical, and software checks, escalate the issue. Contact the supplier and provide the acceptance test data. Be specific. Do not say the machine is slow. Say the cycle time is 20% slower than the rated speed at the specified feed rate.
Request a service visit. If the supplier cannot fix the issue on site, ask for a replacement part or a refund on the affected performance metric. The purchase agreement should define what happens if the machine does not meet spec.
If the supplier is unresponsive, consider a third-party inspection. An independent engineer can measure the machine and provide a report. This report is often persuasive in negotiations.
Do not ignore a small gap. A 0.1 mm tolerance error today can become a 1 mm error tomorrow as the machine wears. Address the issue now. The machine is new. The cost to fix it is low. The cost to live with a gap is high.
Frequently asked questions
Can a machine performance gap be fixed with a software update?
Sometimes. Conservative controller settings or outdated firmware can limit output. Verify the settings against the spec sheet before assuming a hardware fault.
How much runout is acceptable for a CNC spindle?
This varies by machine size and intended application. Check the manufacturer's manual. Generally, higher precision work requires lower runout values.
What should I do if the supplier refuses to acknowledge a gap?
Provide objective data from acceptance testing. Reference the specific clause in the purchase agreement that defines performance requirements.
Is it normal for a new machine to take weeks to reach full performance?
No. A new machine should meet its specs from the first run. Any "break-in" period should be clearly documented in the supplier's instructions.
How do I verify the electrical supply is adequate?
Measure the line voltage at the machine's main breaker. Compare it to the nameplate requirement. Check for voltage drops during full load operation.