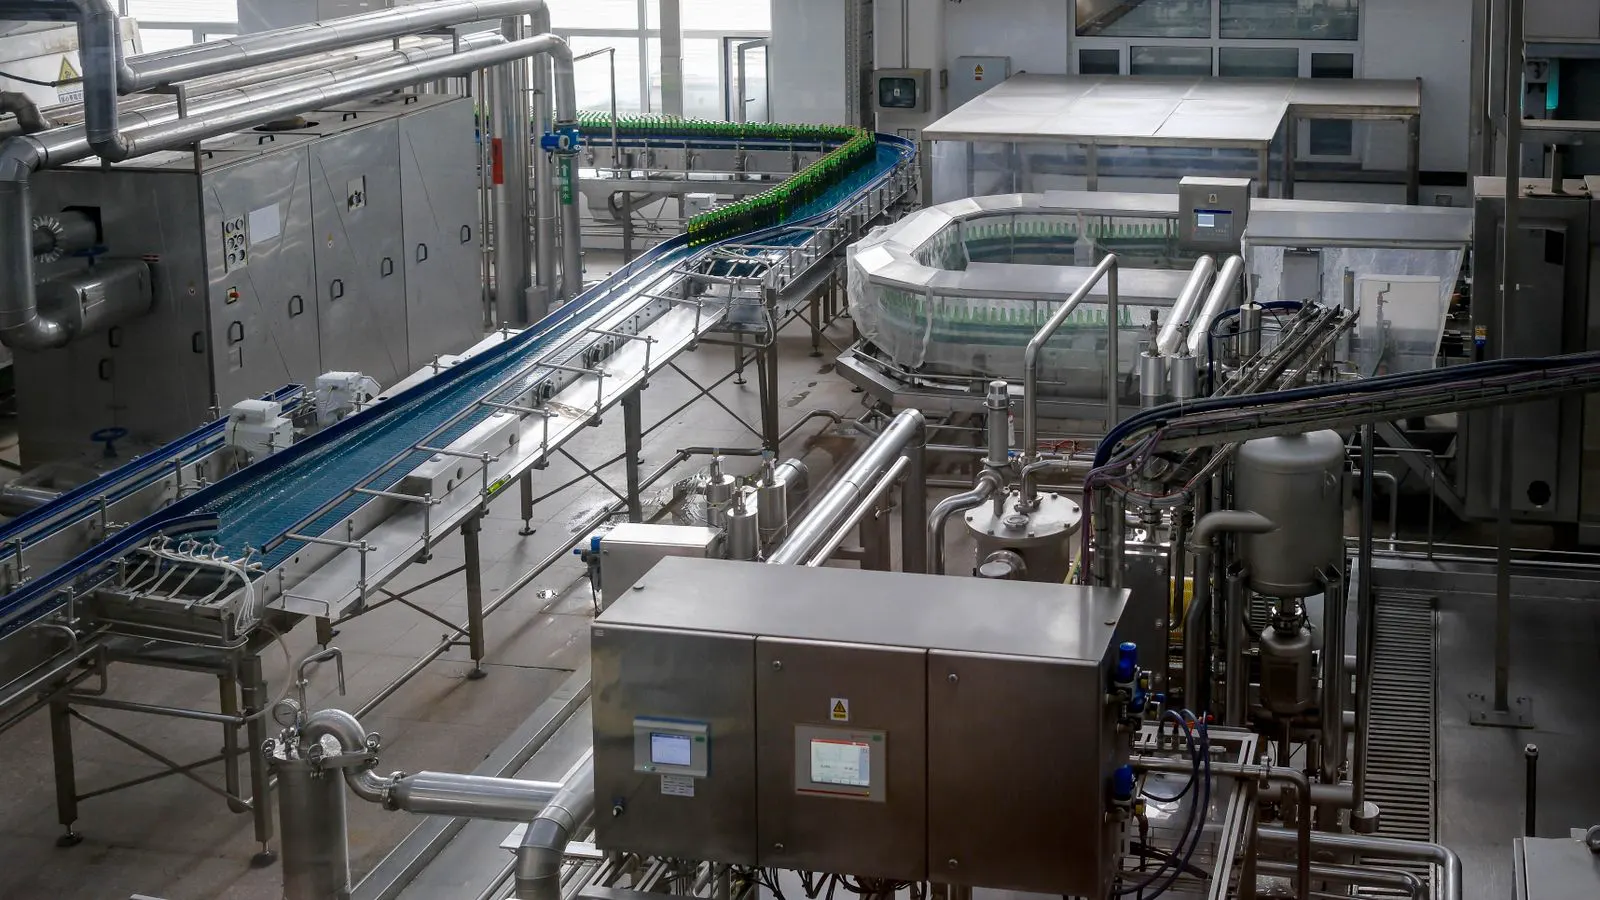
Automated finishing in 2026 changes edge banding machine operation through better sensor integration, line speed control, and data tracking. Buyers should plan for five shifts: smarter glue application, tighter tolerances, predictive maintenance, digital documentation, and flexible changeovers.
- Sensor-based glue control reduces waste and improves bond quality on edge banding machines.
- Line speed synchronization is becoming the main lever for consistent finish quality.
- Predictive maintenance lowers downtime risk on automated finishing lines.
- Digital job data supports traceability and faster setup for mixed production.
- Flexible changeover systems reduce labor time for small batch runs.
What is changing in automated edge finishing
The edge banding machine is no longer just a gluing and trimming station. In 2026, it sits inside a connected finishing chain where glue application, clamping, trimming, and surface treatment are tracked together. The change is visible in the control panel, the glue pot, and the way operators respond to defects.
Buyers now expect the machine to hold tighter tolerances without constant manual correction. A panel that runs through the line at the right speed, with the right glue film and the right pressure, produces a finish that needs less inspection. The machine handles the small variations that used to require operator judgment.
This shift matters because edge work is often the first place customers notice inconsistency. A thin glue line, a slightly lifted edge, or a visible trim mark shows up on the final piece. Automation reduces that risk by making the process more repeatable.
How glue application is becoming more controlled
Glue control is the core of the edge banding machine. In many plants, the operator still sets the pot temperature, the feed rate, and the blade gap by hand. In automated finishing setups, those settings are tied to the job data.
A typical system reads the panel type, the edge band material, and the expected line speed. The glue pot then adjusts the application thickness. If the band is thicker, the system may apply a slightly heavier film. If the panel is a dense hardwood substrate, the system may reduce the film to avoid squeeze-out.
This reduces two common problems. The first is over-application, which creates glue build-up and slows down trimming. The second is under-application, which leaves weak bonds and increases the risk of peeling. When the glue is applied in a narrow range, the trim knife works easier and the finish looks cleaner.
Buyers should check how the machine receives job data. The best systems pull settings from the order file or the central control system. The weaker systems require manual entry for every job. If the plant runs many small batches, manual entry becomes a source of error and delay.
What line speed synchronization means for quality
Line speed is the most practical setting on an edge banding machine. It determines how long the panel stays in the glue zone, the clamp zone, and the trim zone. If the speed changes without adjusting the other stations, the bond quality changes.
In automated finishing, the line speed is no longer a single knob. It is a coordinated value. The glue feed, the roller pressure, and the trim knife timing all respond to the same speed signal. A slower speed gives the glue more time to wet the surface. A faster speed needs more precise feed control to keep the film thin.
The practical result is a more consistent finish. When the speed is stable, the operator spends less time adjusting the trim knife and more time checking the finished edge. When the speed varies, the operator is constantly correcting the trim and cleaning up glue residue.
Buyers should ask how the line speed is controlled. A simple inverter with a speed setpoint is basic. A more advanced setup uses encoder feedback from the main drive and adjusts the glue feed in real time. This keeps the glue film stable even when the line speed changes by a small amount.
How automated inspection changes the finishing workflow
Inspection used to be a manual step. The operator walked the line, checked the edges, and flagged defects to the operator or the next station. Now, automated finishing often includes optical checks at the trim and at the final inspection point.
A typical inspection system looks for three things. It checks for missing band, for glue squeeze-out, and for surface defects on the edge. The system can also measure the edge position and flag panels that are off by a small amount.
This changes the workflow in two ways. First, defects are caught earlier. A panel that has a thin spot in the glue line is flagged before it moves to the next process. Second, the data is recorded. The plant can see which jobs have higher defect rates and which machines need adjustment.
For buyers, the value is in the traceability. If a customer reports a peeling edge on a finished cabinet, the plant can look back at the glue film data and the inspection records. That makes the problem easier to fix. A manual log, by contrast, often gives only a rough picture.
What predictive maintenance looks like on an edge banding machine
Maintenance used to follow a fixed schedule. The operator cleaned the glue pot, checked the rollers, and replaced the trim blade at set intervals. In 2026, automated finishing lines use condition data to schedule maintenance closer to when it is needed.
The machine can monitor the glue pot temperature, the motor load, and the trim knife pressure. If the temperature drifts from the setpoint, the system can flag it. If the motor load rises, the system can suggest a roller check. If the trim knife pressure changes, the system can alert the operator to inspect the blade.
This reduces two risks. The first is a sudden failure during a production run. The second is over-maintenance, where parts are changed too often. The plant can focus on the components that actually show wear.
Buyers should ask what data the machine records. The minimum useful set includes glue pot temperature, line speed, motor current, and trim blade status. A more complete system also includes vibration and pressure data. The more data the system records, the more useful the maintenance alerts become.
How changeover time is being reduced
Small batches are common in furniture and cabinetry. Each job may use a different edge band material, a different glue type, and a different surface finish. In the past, changeover time was a major cost. The operator had to clean the glue pot, swap the band, and adjust the trim.
Automated finishing is reducing that time in two ways. The first is stored job presets. The machine holds the settings for each job type. When the operator selects the job, the glue pot, the line speed, and the trim settings load automatically. The second is cleaner changeover routines. The machine can run a short self-clean cycle that reduces the amount of manual cleaning required.
The practical result is less labor time and fewer setup errors. The operator spends less time adjusting the machine and more time checking the first panels after changeover. For a plant that runs many short jobs, this can change the daily production plan.
Buyers should check how the machine stores presets. The best systems let the operator save a job with a single button and assign it to a material code. The weaker systems require the operator to re-enter every setting. If the plant runs frequent changeovers, this difference matters.
How to prepare your edge banding machine for 2026
The table below shows the main areas where buyers should focus their preparation. Each area has a current practice and a practical step for the next phase.
| Area | Current practice | Preparation step |
|---|---|---|
| Glue application | Manual pot temperature and feed rate | Confirm the machine can receive job data and adjust glue film |
| Line speed | Single speed setpoint with manual trim adjustment | Check how the glue feed and trim timing follow the speed signal |
| Inspection | Manual visual check at the end of the line | Plan for an optical inspection point at the trim or final station |
| Maintenance | Scheduled cleaning and blade change | Review what data the machine records for temperature, load, and blade pressure |
| Changeover | Manual preset entry and cleaning | Test whether the machine stores job presets and runs a self-clean cycle |
The preparation does not require a full line replacement. It starts with the data. If the machine does not record glue film thickness, line speed, or trim position, the plant cannot build a useful automated finishing workflow. The next step is to check how the control system handles job data. A system that pulls settings from the order file is easier to scale than one that requires manual entry.
The second step is to define the inspection point. The plant needs a clear place to check the edge. The trim point is a good place to catch glue and band defects. The final point is a good place to check the finished edge. If the plant only inspects at the end, defects are harder to trace and harder to fix.
The third step is to review maintenance data. The plant should know what the machine records and who looks at the data. If the machine records temperature and motor load but no one reviews the alerts, the data is useless. The maintenance plan should match the data the machine actually provides.
The fourth step is to test changeover. Run a typical job sequence and measure the time from one job to the next. Then test the preset system and the clean cycle. The goal is to reduce the manual steps that cause errors and delay.
The final step is to train the operator. The operator still has to check the first panels and respond to alerts. The role changes from constant adjustment to monitoring and verification. The operator needs to understand what the data means and what action is required when the system flags a problem.
What buyers should ask before purchasing
When comparing an edge banding machine for automated finishing, the questions are specific. The buyer should not only ask about speed and capacity. The buyer should ask how the machine handles the data that drives the process.
The first question is how the glue application responds to job data. Does the glue pot adjust the film thickness based on the band material and the panel type? Does the system flag an out-of-range value?
The second question is how the line speed is coordinated. Does the glue feed and the trim timing follow the same speed signal? Does the system use encoder feedback from the main drive?
The third question is where the inspection point is. Does the machine include an optical check at the trim or at the final station? Does the inspection system record defect data by job?
The fourth question is what maintenance data the machine records. Does it store glue pot temperature, motor load, and trim blade pressure? Does it send alerts to the operator or to a central system?
The fifth question is how changeover works. Does the machine store job presets? Does it run a self-clean cycle? How long does a typical changeover take on the machine the buyer is evaluating?
How to plan the transition
The transition to automated finishing is not a single purchase. It is a set of steps that build on each other. The plant starts with data. It moves to inspection. It moves to predictive maintenance. It moves to flexible changeover.
The first step is to identify the weakest link in the current process. Is the glue application inconsistent? Is the trim quality variable? Is the changeover time too long? The plant should focus on the link that causes the most defects or the most delay.
The second step is to define the data the plant needs. The plant should not collect data for its own sake. The data should support a decision. The operator should be able to look at the data and know what to do next.
The third step is to test the change. Run the new settings on a small batch. Compare the finish quality with the old settings. Measure the time saved and the defects reduced. The plant should not roll out the change across the whole line until the small batch works.
The fourth step is to update the training. The operator needs to know how the new system works. The maintenance team needs to know how to read the alerts. The production manager needs to know how to use the job data for planning.
The fifth step is to review the results after a set period. The plant should compare the defect rate, the changeover time, and the maintenance downtime before and after the change. The review should be practical. The goal is to confirm that the investment is working and to identify the next improvement.
Final practical note
The edge banding machine in 2026 is a data-driven part of the finishing line. The value is not in replacing the operator. The value is in reducing the small variations that create defects and delay. The plant that captures the right data, inspects at the right point, and trains the operator to use the alerts will get a cleaner finish and a more stable production plan.
The buyer should focus on the process, not just the machine. The machine is only as useful as the data it provides and the way the plant uses that data. A well-configured edge banding machine with a clear inspection point and a simple data review will outperform a larger machine with no data support.
Frequently asked questions
What is the most important change in automated edge finishing for 2026?
The most important change is that the edge banding machine now coordinates glue application, line speed, and trim timing from a single job data set. This reduces the manual adjustments that used to create finish variation.
Does automated finishing replace the operator on the edge banding machine?
No. The operator still checks the first panels, responds to alerts, and handles changeovers. The role shifts from constant manual adjustment to monitoring and verification.
What data should a buyer expect from a modern edge banding machine?
The minimum useful data set includes glue pot temperature, line speed, glue film thickness, and trim position. More advanced systems also include motor load, vibration, and inspection defect records.
How can a plant reduce changeover time on an edge banding machine?
The plant should use stored job presets and a self-clean cycle. The operator selects the job, and the machine loads the glue, speed, and trim settings. The clean cycle reduces manual cleaning time.
What is the first step to prepare for automated finishing?
The first step is to identify the weakest link in the current process, such as glue application or trim quality. Then define the data the plant needs to improve that link.


