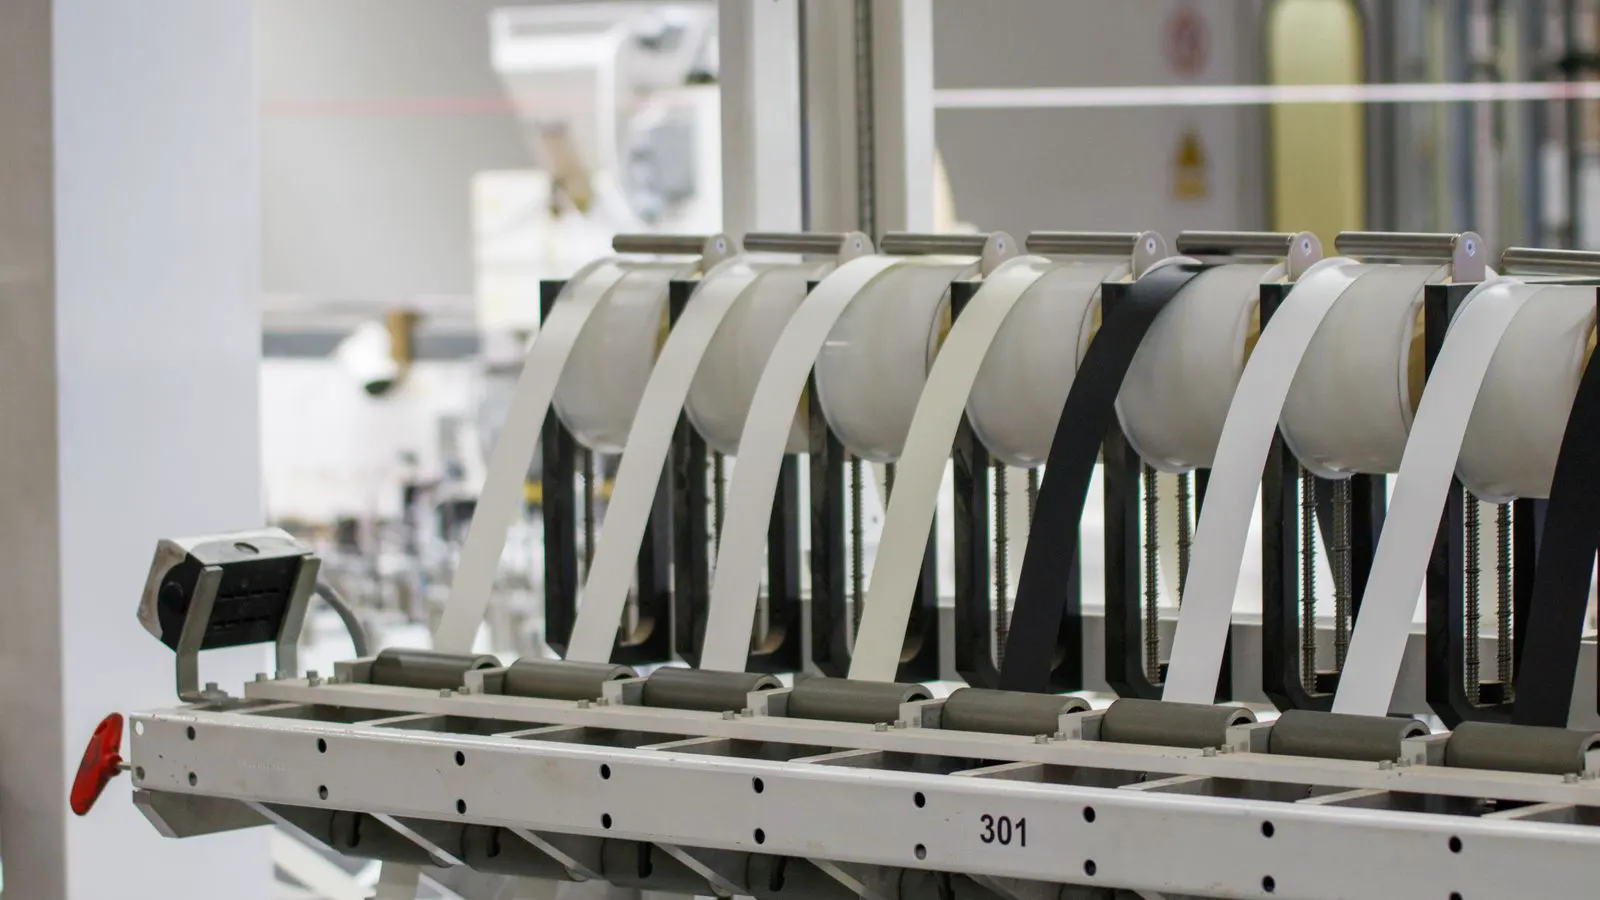
Next-generation edge adhesive technology shifts toward solvent-free chemistries, digital bonding controls, and tighter compatibility with engineered wood. Operators should plan for faster cure times, stricter line speed discipline, and updated maintenance routines for modern edge banding lines.
- Edge adhesive chemistry is moving away from solvent-heavy systems toward low-odor and low-VOC options.
- Line speed and temperature control are now as important as adhesive type for reliable panel edge bonding.
- Operators should verify adhesive compatibility with veneer, foil, ABS, and MDF edges before changing brands.
- Maintenance schedules need updating to handle new pot materials and cleaning solvents.
- Future-proofing an edge banding line means planning for digital controls and data-driven adhesive management.
Modern edge banding lines are under pressure to run cleaner, faster, and with less waste. Plant managers are watching VOC limits, shop air quality, and material costs all at once. The adhesive in the pot is often the first place where problems show up.
This outlook covers five shifts buyers and engineers should plan for as the next generation of edge adhesive technology matures. The focus is practical. How do these changes affect machine setup, maintenance, quality control, and long-term production reliability?
What is changing in adhesive chemistry
The biggest change is moving away from solvent-based systems. Many plants are evaluating water-based or solvent-free edge adhesive options. These systems reduce fumes and simplify cleanup. They also tend to have slower cure times at low temperatures, which can change how operators manage the line.
Solvent-free chemistries are often formulated to bond a broader range of panel materials. They work well on MDF, particleboard, and laminated edges. They can also handle foils and some plastic veneers. The trade-off is that some formulations are less forgiving during short production runs.
Plant engineers should treat every adhesive change as a controlled test. Do not assume a new edge adhesive behaves like the old one. Run a small batch. Check the joint under heat, friction, and moisture stress. Keep the first ten panels for inspection.
Water-based systems often require tighter control of the adhesive pot temperature. If the pot runs too cool, the bond weakens. If it runs too hot, the adhesive can dry out before it reaches the panel edge. Operators need to monitor temperature more often.
How line speed and temperature affect bonding
A common mistake is focusing only on the adhesive label and ignoring machine settings. Edge adhesive performance depends heavily on line speed, adhesive temperature, and pressure. The next generation of adhesives is more sensitive to these variables.
Faster line speeds can reduce contact time. If the adhesive does not have enough time to wet the panel edge and the banding material, the bond may fail later. Slower speeds help, but they can also increase drying risk if the adhesive is exposed to air too long.
Temperature is the other major variable. Warm plant conditions can help a water-based adhesive flow and bond. Cold conditions can slow cure and increase the risk of delamination. Plants with climate control should use that advantage. Plants without climate control should plan for seasonal adjustments.
The table below shows how common variables affect bonding quality.
| Variable | Effect on bond | Typical operator response |
|---|---|---|
| Line speed too high | Short contact time, weak wetting | Reduce speed or increase pressure |
| Pot temperature too low | Poor flow, dry edges | Raise temperature within safe range |
| Pot temperature too high | Premature drying, clogging | Lower temperature, clean pot |
| Pressure too low | Incomplete contact | Adjust nip pressure |
| Ambient temperature too low | Slow cure, weak early bond | Insulate area or adjust pot |
Buyers should ask suppliers about the minimum and maximum line speeds for a given edge adhesive. Do not rely on a single number. Ask for a range and the conditions that support it.
What panel edge and banding material compatibility means
Not every edge adhesive performs the same way on every panel edge. MDF, particleboard, laminates, and engineered wood have different surface energies. Some surfaces absorb moisture. Others repel it. Foil and ABS edges behave differently from wood veneer.
A new adhesive may bond well on a standard wood veneer but fail on a plastic edge. The plant must test compatibility across all materials in use. This is especially true when changing from solvent-based to solvent-free systems.
Panel edge preparation also matters. A rough or dusty edge rejects adhesive. Scraping, sanding, and cleaning are part of the bonding process. If the edge is not clean, no adhesive will save the joint.
Engineers should create a simple compatibility matrix for the shop. List each panel material, banding material, and adhesive brand. Record the test result. Keep the matrix updated. This becomes a reference when troubleshooting delamination or peeling.
What maintenance changes look like
New edge adhesive systems often require different cleaning routines. Solvent-based adhesives may leave residue that needs a strong solvent. Water-based systems may dry into a film that needs water or a mild cleaner. Some low-VOC systems require a specific cleaner.
Pot maintenance is more critical with newer chemistries. If the adhesive dries in the pot, it can clog the heater and the feed system. Plants should check the pot at the start and end of each shift. They should also inspect the nozzles and pressure seals.
The cleaning schedule should match the adhesive type. Do not use a harsh chemical on a water-based system unless the supplier says it is safe. Do not use water on a solvent-based system unless it is designed for that. Mixing cleaning methods can damage the pot or reduce bond strength.
Maintenance records should include adhesive lot numbers, cleaning chemicals, and temperature readings. This creates a paper trail. If a batch fails, the plant can trace the problem back to a specific adhesive lot or a temperature drift.
What digital controls and data logging will do
The next generation of edge adhesive technology is also connected to machine controls. Many newer edge banding machines allow operators to log adhesive temperature, line speed, and pressure in real time. Some systems store this data for later review.
This changes how plants troubleshoot. Instead of guessing, they can compare good batches with bad batches. They can see if a delamination problem started after a temperature drop or a speed increase. They can adjust settings based on data, not habit.
Buyers should ask whether the machine supports digital adhesive management. Can the operator save a recipe for each banding material? Can the system warn if the pot temperature goes out of range? Can the machine log the data to a local drive or a network server?
These features are not just convenience. They help maintain consistency. They also support quality audits. If a customer reports a peeling edge, the plant can look at the machine data and see if anything changed during that run.
How to prepare your edge banding line for the next generation
Preparing for new edge adhesive technology is not a one-time project. It is a series of small changes.
- Audit the current adhesive. Check the data sheet. Note the cure time, temperature range, and cleaning requirements.
- Test one new adhesive on a small scale. Use the same panel and banding materials. Run at normal line speed.
- Review machine settings. Check line speed, pressure, and pot temperature. Adjust based on the test.
- Update the maintenance schedule. Add cleaning steps and inspection points for the new adhesive.
- Train operators. Teach them to read the machine data and recognize early signs of bonding failure.
- Keep a compatibility log. Record which adhesives work well with which materials.
The goal is not to chase every new product. The goal is to build a process that can adapt. A well-run edge banding line can switch adhesive brands without losing quality. It can handle new chemistries without guessing.
Final outlook for edge banding operations
Edge adhesive technology is moving toward cleaner, more controllable, and more data-driven systems. The next few years will bring more options, not fewer. Plants that prepare now will have an easier transition.
The key is to treat adhesive selection as part of the whole line, not just a consumable. The right edge adhesive depends on panel material, banding material, line speed, temperature, and maintenance. When those factors are aligned, the bond holds. When they are not, the edge fails.
Buyers and engineers should plan for these changes. Test new adhesives carefully. Update maintenance routines. Use machine data to guide decisions. The edge banding line of the future will be cleaner, faster, and more reliable. The plants that get there first will be the ones that treat the adhesive as a critical part of the process.
Frequently asked questions
Can a plant switch to a water-based edge adhesive without changing the machine?
Often yes, but the machine settings may need adjustment. Check the adhesive data sheet for temperature and line speed limits, then run a small test batch.
What is the biggest risk when changing edge adhesive?
The biggest risk is assuming the new adhesive behaves like the old one. Always test on the same panel and banding materials used in production.
How does line speed affect edge adhesive bonding?
Too fast reduces contact time and can weaken the bond. Too slow can increase drying risk. The adhesive data sheet should list a safe speed range.
What maintenance changes are needed for solvent-free edge adhesive?
Cleaning routines may change. Use the cleaner recommended by the adhesive supplier. Check the pot more often for drying or clogging.
Should plants buy new edge banding machines to handle future adhesives?
Not always. Many newer adhesives can run on existing machines if the settings and maintenance are updated. Buy new equipment only if the current machine cannot meet the new process needs.


